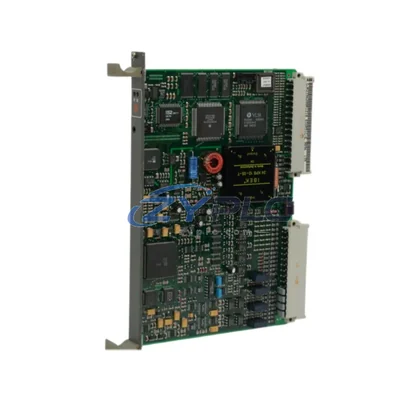
ABB HIEE451116R0001 FM9925A-E: Industrial Data Link for Smart Factory Connectivity
The ABB HIEE451116R0001 FM9925A-E is a high-performance industrial communication gateway and circuit board designed for the FM9925A Series, engineered to serve as the critical data bridge between field-level devices and upper-level control and monitoring systems. In modern smart factory environments, seamless and reliable data flow across every layer of the automation hierarchy is non-negotiable — and the HIEE451116R0001 FM9925A-E delivers exactly that, enabling real-time signal acquisition, multi-protocol conversion, and stable network transmission across complex industrial topologies.
From the moment a sensor detects a process variable on the plant floor, the data journey begins. The FM9925A-E module captures signals from field instruments and transmits them upward through the automation stack — through PLCs, remote I/O modules, HMI panels, SCADA servers, and ultimately to MES and ERP platforms. This end-to-end connectivity eliminates data silos, reduces manual intervention, and gives plant engineers full visibility into production status in real time.
Compatibility & Integration Notes
| Parameter |
Specification |
| SKU |
HIEE451116R0001 FM9925A-E |
| Brand |
ABB |
| Series |
FM9925A |
| Product Type |
Industrial Communication Gateway / Circuit Board |
| Protocol Support |
PROFIBUS DP, PROFINET, Modbus RTU, Modbus TCP/IP, DeviceNet, EtherNet/IP |
| Interface Types |
RS-232, RS-485, RJ45 Ethernet, Fiber Optic (optional) |
| Transmission Capability |
Real-time cyclic and acyclic data exchange; deterministic low-latency communication |
| Network Compatibility |
Compatible with ABB AC500, AC800M, and Symphony Plus DCS platforms |
| System Applications |
SCADA, DCS, HMI, MES, Remote I/O, Drive Networks, Safety Systems |
| Operating Temperature |
-20°C to +70°C |
| Power Supply |
24 VDC (standard industrial rail) |
| Certifications |
CE, UL, RoHS compliant |
| Origin |
Sweden |
| Warranty |
warranty terms confirmed during quotation | Tested before shipment |
Connected Automation Data Flow
The HIEE451116R0001 FM9925A-E sits at the heart of a layered industrial network architecture. At the field level, it interfaces directly with distributed sensors, pressure transmitters, flow meters, and temperature probes — collecting raw process data and converting analog or digital signals into structured network packets. These packets are then routed upward through the communication backbone to ABB AC500 PLCs and AC800M controllers, which execute the core logic of the automation program.
Within the same network segment, the FM9925A-E communicates seamlessly with ABB CI854A PROFIBUS DP communication interfaces and CI871K PROFINET adapter modules, enabling high-speed cyclic data exchange between the controller and remote I/O clusters. Remote I/O stations — such as the ABB S900 remote I/O series — can be distributed across large plant areas while maintaining deterministic, low-latency communication back to the central controller through the FM9925A-E gateway.
At the HMI and SCADA layer, the module feeds real-time process data to ABB CP600 HMI panels and integrates with ABB System 800xA SCADA/DCS platforms, providing operators with live dashboards, alarm management, and trend analysis. The FM9925A-E also supports integration with third-party SCADA systems via standard Modbus TCP/IP and OPC-UA protocols, making it a versatile gateway in mixed-vendor environments.
For drive networks, the module connects to ABB ACS880 variable frequency drives and ACS580 drives via PROFIBUS DP or PROFINET, enabling closed-loop speed and torque control with real-time feedback. In safety-critical applications, it can interface with ABB Pluto safety PLCs and safety I/O modules, ensuring that safety data is transmitted with the required integrity and response time.
Edge computing and remote diagnostics are also supported through integration with ABB Ability Edge gateways, which aggregate data from the FM9925A-E and push it to cloud-based analytics platforms for predictive maintenance, OEE monitoring, and energy management. Industrial power supplies from the ABB CP-E series provide stable 24 VDC power to the communication module and connected field devices, ensuring uninterrupted operation even in harsh industrial environments.
Solving Data Isolation in Industrial Sites
One of the most persistent challenges in industrial automation is the coexistence of legacy equipment running older protocols alongside modern Ethernet-based systems. The ABB HIEE451116R0001 FM9925A-E directly addresses this challenge by acting as a multi-protocol bridge — translating between PROFIBUS DP, Modbus RTU, DeviceNet, and PROFINET/EtherNet/IP without requiring costly infrastructure overhauls.
Data silos — where information is trapped within isolated subsystems and cannot be accessed by upper-level management or analytics platforms — are eliminated through the FM9925A-E’s transparent data routing capabilities. Process variables from field instruments, status registers from PLCs, and diagnostic data from drives are all aggregated and made available to SCADA, MES, and ERP systems in a unified, structured format.
Remote monitoring and diagnostics become straightforward with the FM9925A-E in place. Plant engineers can access real-time device status, communication health metrics, and alarm logs from any authorized workstation on the network — or remotely via secure VPN connections — without needing to be physically present on the plant floor. This capability is especially valuable for multi-site operations where centralized monitoring of geographically distributed facilities is required.
Production line transparency is another key benefit. With the FM9925A-E connecting every layer of the automation hierarchy, production managers gain access to live OEE data, cycle time metrics, and quality indicators — enabling data-driven decisions that reduce downtime, improve throughput, and support continuous improvement initiatives. System expansion is equally straightforward: the modular architecture of the FM9925A Series allows additional communication modules to be added as production lines grow, without disrupting existing network configurations.
Every unit of the HIEE451116R0001 FM9925A-E supplied by ZYPLC undergoes pre-shipment functional testing to verify communication integrity, protocol compatibility, and hardware performance. Stock is maintained for shipment arranged after confirmation, and all units are covered by a warranty terms confirmed during quotation from the date of delivery.
Industrial Connectivity FAQ
Q1: What is the communication latency of the ABB HIEE451116R0001 FM9925A-E in a PROFINET network?
A: In a standard PROFINET RT (Real-Time) configuration, the FM9925A-E supports cycle times as low as 1 ms, ensuring deterministic data exchange suitable for motion control and high-speed process automation applications. Actual latency depends on network topology, number of nodes, and controller scan cycle settings.
Q2: Is the FM9925A-E compatible with third-party PLCs and SCADA systems outside the ABB ecosystem?
A: Yes. The HIEE451116R0001 FM9925A-E supports open industrial protocols including Modbus TCP/IP, Modbus RTU, and PROFIBUS DP, which are widely supported by Siemens, Schneider Electric, Rockwell Automation, and other major automation vendors. OPC-UA connectivity further extends compatibility with modern SCADA and MES platforms from any manufacturer.
Q3: How does ZYPLC ensure network stability and hardware reliability for the FM9925A-E?
A: Each unit undergoes a comprehensive pre-shipment test protocol that includes communication loop testing, protocol handshake verification, and thermal stress screening. Units that pass all test criteria are shipped with a test report and are covered by a warranty terms confirmed during quotation. ZYPLC maintains buffer stock of the FM9925A-E to support urgent project timelines and emergency replacement requirements.
Q4: Can the ABB FM9925A-E be used to expand an existing automation network without reconfiguring the entire system?
A: Yes. The FM9925A Series is designed for modular scalability. The HIEE451116R0001 FM9925A-E can be added to an existing FM9925A rack or communication backplane without requiring changes to the controller program or network addressing scheme, provided the new module is configured with a unique node address. This makes it ideal for phased expansion projects where production continuity is a priority.
—