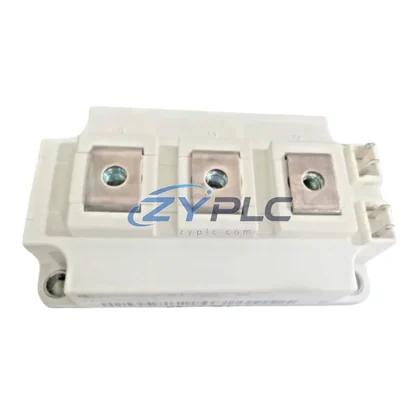
ABB SNAT7600 Industrial Network Interface for ACS600 Systems: Powering the Industrial Data Link in Smart Factory Environments
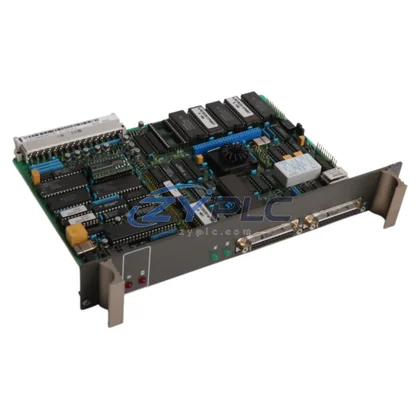
The ABB SNAT7600 is a high-performance IGBT control board engineered specifically for the ACS600 series of AC drives. Far beyond a simple replacement component, the SNAT7600 functions as the central intelligence layer within the ACS600 drive architecture — managing gate-level IGBT switching logic, real-time feedback loops, and multi-protocol communication bridging that connects field-level power devices to upper-layer automation systems. In modern smart factory deployments, where every millisecond of data latency and every point of network interoperability matters, the SNAT7600 delivers the connectivity backbone that keeps production lines transparent, responsive, and continuously optimized.
Compatibility & Integration Notes
| Parameter |
Specification |
| SKU |
SNAT7600 |
| Brand |
ABB |
| Compatible Series |
ACS600 |
| Product Type |
IGBT Control Board / Industrial Network Interface |
| Supported Protocols |
Profibus-DP, Modbus RTU, Modbus TCP/IP |
| Interface Types |
Fieldbus adapter slot, serial RS-485, digital I/O |
| Transmission Capability |
Real-time cyclic data exchange, parameter read/write, fault diagnostics |
| Network Compatibility |
Profibus networks, Modbus master/slave topologies, DCS integration |
| System Applications |
SCADA, DCS, PLC-controlled drive systems, HMI monitoring, remote diagnostics |
| Origin |
Finland (ABB OEM) |
| Warranty |
warranty terms confirmed during quotation — Tested before shipment |
Connected Automation Data Flow
In a fully integrated smart factory, the ABB SNAT7600 sits at the intersection of power conversion and data communication. The data flow begins at the sensor and actuator layer: process sensors — including temperature transmitters, pressure transducers, and encoder feedback units — feed real-time signals into the ACS600 drive. The SNAT7600 control board processes these inputs at the gate-drive level, executing precise IGBT switching sequences that regulate motor torque, speed, and energy consumption with microsecond accuracy.
From the drive level, the SNAT7600 communicates upstream via Profibus-DP to a Siemens S7-300 or S7-400 PLC, or alternatively through Modbus RTU to an Allen-Bradley MicroLogix or CompactLogix controller. These PLCs aggregate drive status data — including output frequency, DC bus voltage, motor current, and active fault codes — and relay it to the plant’s SCADA system (such as Wonderware InTouch or Ignition by Inductive Automation) for real-time visualization and historical trending.
For facilities using distributed I/O architectures, the SNAT7600-equipped ACS600 drive integrates seamlessly with ABB CI854 Profibus communication modules and remote I/O stations such as the ABB S800 I/O series, enabling decentralized control without sacrificing data fidelity. HMI panels — including ABB CP600 series operator panels — can display live drive parameters, acknowledge alarms, and initiate start/stop sequences directly through the Profibus network managed by the SNAT7600.
In multi-drive installations, the SNAT7600 supports coordinated operation across several ACS600 units, with each drive node addressable on the Profibus segment. This architecture is particularly valuable in conveyor systems, pump stations, compressor banks, and multi-axis winding lines where synchronized speed control and load sharing are critical. The ABB RDCO-02 or RDCO-03 communication option boards can be paired with the SNAT7600 to extend connectivity to fiber-optic drive-to-drive links, further enhancing noise immunity in high-interference industrial environments.
At the edge layer, data from the SNAT7600 can be aggregated by an industrial edge gateway — such as the ABB Ability Edge or a third-party IIoT gateway — enabling cloud-based analytics, predictive maintenance algorithms, and OEE (Overall Equipment Effectiveness) dashboards. This end-to-end data chain — from IGBT gate signal to cloud analytics — is made possible by the SNAT7600’s robust communication architecture and its compatibility with the broader ABB automation ecosystem.
Solving Data Isolation in Industrial Sites
One of the most persistent challenges in legacy industrial environments is protocol fragmentation: drives, PLCs, sensors, and SCADA systems from different generations and vendors often speak incompatible communication languages, creating data silos that prevent plant-wide visibility. The ABB SNAT7600 directly addresses this by supporting both Profibus-DP and Modbus protocols within the ACS600 platform, acting as a protocol bridge that unifies drive-level data with higher-level control and monitoring systems.
For facilities struggling with remote monitoring limitations, the SNAT7600 enables full parameter transparency over the fieldbus network — operators can read motor speed, output current, fault history, and energy consumption from a central SCADA workstation without physically accessing the drive cabinet. This capability is essential for unmanned substations, remote pump stations, and geographically distributed production lines.
Production line transparency is further enhanced by the SNAT7600’s real-time fault reporting. When an IGBT overcurrent event, DC bus overvoltage, or thermal overload occurs, the board immediately transmits a structured fault code to the PLC and SCADA system, triggering alarm sequences and enabling rapid root-cause analysis. This eliminates the diagnostic delays that occur when fault data is trapped inside the drive and inaccessible to the control room.
For system expansion, the SNAT7600’s modular design within the ACS600 platform allows new drive nodes to be added to an existing Profibus segment with minimal reconfiguration. Engineering teams can commission additional drives, assign new Profibus node addresses, and integrate them into the existing SCADA topology without redesigning the communication architecture — a significant advantage for phased capacity expansions in automotive, chemical, and water treatment plants.
Every ABB SNAT7600 unit supplied by ZYPLC undergoes functional testing prior to shipment, verifying IGBT gate drive signals, communication port integrity, and power supply regulation. Stock is maintained in our warehouse to support urgent maintenance requirements, with same-day dispatch available for availability confirmed by RFQ units.
Industrial Connectivity FAQ
Q1: What communication protocols does the ABB SNAT7600 support, and is it compatible with my existing PLC network?
The SNAT7600 supports Profibus-DP and Modbus RTU/TCP protocols through the ACS600 drive’s fieldbus adapter interface. It is compatible with Siemens S7 series PLCs via Profibus, and with Allen-Bradley, Schneider, and other Modbus-capable controllers. For other protocols such as DeviceNet or EtherNet/IP, an appropriate ABB fieldbus adapter module (e.g., RDNA-01 for DeviceNet) can be installed alongside the SNAT7600.
Q2: What is the typical communication latency for real-time drive control via Profibus-DP using the SNAT7600?
Profibus-DP cyclic communication with the ACS600 drive via the SNAT7600 typically achieves cycle times of 1–10 ms depending on the number of nodes on the segment and the baud rate configured (up to 12 Mbps). This latency is well within the requirements for closed-loop speed and torque control in most industrial applications, including conveyor synchronization, pump control, and compressor regulation.
Q3: How does the SNAT7600 support network stability in high-interference industrial environments?
The SNAT7600 is designed to ABB’s industrial EMC standards, with shielded signal paths and robust noise filtering on all communication interfaces. In environments with high electromagnetic interference — such as near large motors, welding equipment, or variable-speed drives — the use of shielded Profibus cables and proper grounding of the cable shield at one end of each segment is recommended. The SNAT7600’s onboard diagnostics also monitor communication health and report bus errors to the PLC, enabling proactive network maintenance.
Q4: What warranty and testing does ZYPLC provide with the ABB SNAT7600?
All ABB SNAT7600 units supplied by ZYPLC carry a warranty terms confirmed during quotation covering manufacturing defects and functional failures under normal operating conditions. Each unit is tested before shipment to verify IGBT gate drive functionality, communication port operation, and power supply output. Availability is confirmed via RFQ for same-day or next-day dispatch to minimize production downtime. For urgent requirements, please contact our technical sales team directly.