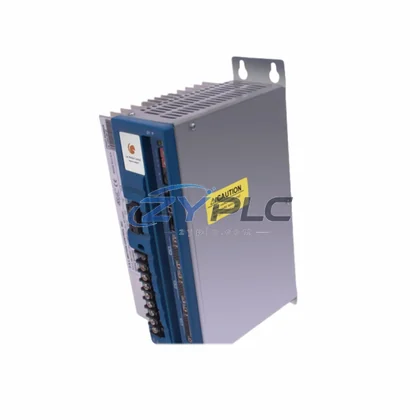
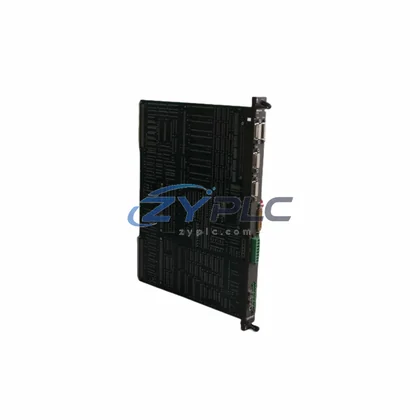
Rexroth VT-HNC100-1-14/134 Digital Axis Controller for VT Automation
The Bosch Rexroth VT-HNC100-1-14/134 is a high-performance digital axis controller engineered for precision motion control in demanding industrial automation environments. Designed within Rexroth’s VT series platform, this controller delivers closed-loop axis positioning with exceptional repeatability, enabling production lines to operate at peak efficiency while minimizing unplanned downtime risk. Whether integrated into hydraulic servo systems, electrohydraulic press lines, or multi-axis forming machines, the VT-HNC100-1-14/134 provides the control intelligence needed to reduce idle-state power draw, shorten cycle times, and extend the operational lifespan of connected actuators and drives.
Product Specification Table
| Parameter |
Specification |
| SKU / Model |
VT-HNC100-1-14/134 |
| Brand / Series |
Bosch Rexroth / VT Series |
| Product Type |
Digital Axis Controller |
| Control Mode |
Closed-loop digital axis positioning |
| Power Consumption |
Low-standby intelligent power management |
| Operating Efficiency |
High-precision servo loop, minimized unplanned downtime |
| Compatible Systems |
Rexroth VT series hydraulic amplifiers, IndraDrive servo drives, BODAS control platforms |
| Application Environment |
Hydraulic press, injection molding, forming machines, industrial automation |
| Value |
Reduces idle-state hydraulic energy loss; optimizes valve response timing |
| Origin |
Germany (DE) |
| Warranty |
warranty terms confirmed during quotation |
| Stock Status |
RFQ Available – Ships within 3–5 business days |
System Compatibility and Application
In a modern industrial automation system, the VT-HNC100-1-14/134 functions as the central intelligence layer between the machine controller and the hydraulic actuation system. It receives position and velocity setpoints from an upstream PLC — such as the Rexroth IndraLogic XLC or a Siemens S7-1500 — and translates them into precise valve control signals that minimize overshoot, reduce pressure spikes, and eliminate unnecessary pump loading. This tight control loop directly reduces the energy demanded from the hydraulic power unit during each machine cycle.
When paired with a Rexroth IndraDrive C or IndraDrive M servo drive on the pump motor, the VT-HNC100-1-14/134 enables coordinated speed-pressure profiling: the pump motor ramps down during low-demand phases of the press cycle, and the axis controller compensates with predictive feedforward to maintain positional accuracy. This combination can reduce hydraulic system operating load by Actual operating results depend on the installed system, load profile, and commissioning parameters.
The controller communicates via PROFIBUS DP or analog interfaces, making it compatible with Rexroth’s IndraControl L65 and L75 motion controllers, as well as third-party SCADA platforms. For condition monitoring, it can be integrated alongside Rexroth’s HMI terminals — such as the IndraControl VCP or VEP series — to display real-time axis load, cycle operating load, and valve duty cycle data. This visibility allows process engineers to identify energy hotspots within the production line without requiring additional power meters.
In multi-axis press lines, the VT-HNC100-1-14/134 is often deployed alongside Rexroth VT-VSPA2 proportional amplifier cards and VT-HACD axis control modules to manage synchronized hydraulic cylinders. The digital communication between these components eliminates analog signal degradation, ensuring that each axis responds identically to setpoint changes — a critical factor in reducing scrap rates and the unplanned downtimed on rework cycles. Complementary I/O expansion modules from the Rexroth Inline or Axioline families can be added to monitor pressure transducers, temperature sensors, and flow meters, feeding data back into the control loop for adaptive maintenance planning.
For facilities implementing ISO 50001 maintenance planning systems, the VT-HNC100-1-14/134 provides the granular axis-level data needed to establish energy performance indicators (EnPIs) for individual machine operations. When combined with a Rexroth BODAS RC controller or an condition monitoring gateway, historical cycle data can be logged and analyzed to identify drift in valve efficiency — an early indicator of seal wear or contamination that, if left unaddressed, leads to increased pump loading and higher energy bills.
Maintenance and Replacement Notes
On a typical hydraulic press line running three shifts, uncontrolled axis motion accounts for a significant share of total unplanned downtime. Pressure relief valve losses, cylinder overshoot, and extended dwell times at full system pressure all contribute to energy that is converted to heat rather than useful work. The VT-HNC100-1-14/134 addresses each of these loss mechanisms through its adaptive closed-loop control algorithm.
By profiling the velocity ramp of the hydraulic cylinder during approach, pressing, and retract phases, the controller reduces peak flow demand on the hydraulic power unit. Lower peak flow means the pump motor operates closer to its efficiency curve for a greater proportion of each cycle, reducing both electrical operating load and thermal load on the hydraulic fluid. Cooler fluid viscosity is more stable, which in turn improves valve response consistency and reduces the frequency of filter maintenance — a direct reduction in planned downtime and maintenance labor costs.
In injection molding applications, where the VT-HNC100-1-14/134 is used to control injection and clamping axes, the controller’s position feedback loop enables precise end-of-stroke deceleration. This eliminates the hydraulic shock that causes premature wear on cylinder seals and manifold connections. Fewer seal replacements mean less unplanned downtime, and the energy that would have been dissipated in shock absorption is instead recovered through controlled deceleration profiling.
Predictive maintenance integration is another key maintenance planning pathway. By monitoring the integral of valve control current over time, the VT-HNC100-1-14/134 can detect increasing valve hysteresis — a sign of spool wear or contamination. Maintenance teams can schedule valve service during planned shutdowns rather than responding to emergency failures, keeping the production line running at its designed energy efficiency level rather than degrading gradually as valve performance deteriorates.
All units supplied by ZYPLC are tested prior to shipment, with functional verification of the closed-loop control response, communication interface integrity, and power supply regulation. Each VT-HNC100-1-14/134 is covered by a warranty terms confirmed during quotation from the date of delivery, with technical support available for integration and commissioning queries.
Product Sourcing FAQ
Q1: How does the VT-HNC100-1-14/134 reduce operating load compared to a conventional analog axis controller?
The VT-HNC100-1-14/134 uses a digital closed-loop algorithm that profiles axis velocity and position in real time, reducing overshoot and eliminating unnecessary pressure hold phases. This directly lowers the average flow demand on the hydraulic pump motor, reducing electrical operating load per cycle compared to analog controllers that rely on fixed gain settings and cannot adapt to load variations.
Q2: Is the VT-HNC100-1-14/134 compatible with existing Rexroth VT series proportional valves and amplifier cards?
Yes. The VT-HNC100-1-14/134 is designed for integration within the Rexroth VT series ecosystem and is compatible with VT-VSPA2 proportional amplifier cards, VT-HACD axis control modules, and standard Rexroth proportional directional valves. It can also interface with third-party valves via analog command outputs, subject to signal range compatibility verification.
Q3: What is the recommended replacement or upgrade path if the original VT-HNC100-1-14/134 is no longer available?
For applications requiring a direct replacement, ZYPLC supports RFQ sourcing for tested VT-HNC100-1-14/134 units sourced from verified supply channels. For new machine designs, Rexroth’s current-generation IndraMotion MLC or BODAS RC platforms offer equivalent axis control functionality with enhanced condition monitoring capabilities. Our technical team can advise on the most cost-effective path based on your existing machine architecture.
Q4: What does the warranty terms confirmed during quotation cover, and what is the testing process before shipment?
Every VT-HNC100-1-14/134 supplied by ZYPLC undergoes pre-shipment functional testing that verifies closed-loop control response, communication interface operation, and internal power supply regulation. The warranty terms confirmed during quotation covers defects in materials and workmanship under normal operating conditions. Warranty claims are supported by our technical team, with replacement or repair turnaround coordinated to minimize production downtime.