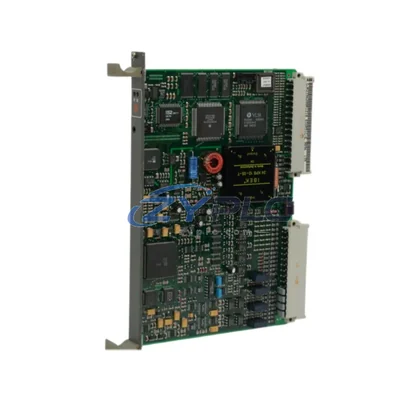
Siemens A5E01708486 Signal Control Board for Perfect Harmony Automation
The Siemens A5E01708486 is a high-performance signal control board engineered for the Perfect Harmony medium-voltage (MV) drive series — one of Siemens’ most advanced variable frequency drive platforms for industrial power management. Designed to serve as the central signal processing and feedback coordination unit within the drive’s control architecture, the A5E01708486 plays a critical role in reducing unplanned downtime risk, stabilizing motor output, and enabling real-time process optimization across demanding production environments.
In modern industrial facilities where energy costs represent a significant share of operating expenditure, the precision of signal control directly determines how efficiently a drive system responds to load changes. The A5E01708486 ensures that the Perfect Harmony drive receives clean, accurately timed control signals — eliminating signal latency that can cause motor over-speed, torque oscillation, or unnecessary reactive power draw. By maintaining signal integrity at the board level, this component contributes to measurable reductions in kWh consumption per production cycle.
Product Specification Table
| Parameter |
Specification / Value |
| Part Number / SKU |
A5E01708486 |
| Compatible Drive Series |
Siemens Perfect Harmony MV Drive (GH180 / NXG) |
| Component Type |
Signal Control Board (PCB) |
| Operating Voltage Range |
Medium Voltage (2.3 kV – 13.8 kV system level) |
| Signal Processing Function |
Feedback coordination, control signal routing, drive-to-PLC interface |
| Maintenance Planning Role |
Reduces signal-induced torque ripple; supports energy-efficient motor speed regulation |
| Compatible Control Systems |
Siemens NXG Controller, SIMATIC S7 PLC series, PROFIBUS / PROFINET networks |
| Application Environments |
Pumps, fans, compressors, conveyors, mills — heavy industrial & process industries |
| Energy Saving Value |
Enables VFD-based speed control; typical operational stability 20–50% vs. fixed-speed operation |
| Origin |
Germany (Siemens Industrial Manufacturing) |
| Warranty |
warranty terms confirmed during quotation | Tested before shipment |
| Stock Status |
RFQ Available — shipment arranged after confirmation |
System Compatibility and Application
The A5E01708486 does not operate in isolation — it functions as a precision node within a broader industrial automation system. In a typical Perfect Harmony installation, the signal control board interfaces directly with the Siemens NXG Controller, which serves as the master control unit for the entire MV drive system. The NXG controller issues speed reference commands and torque setpoints; the A5E01708486 processes and routes these signals to the power cell modules with microsecond-level accuracy, ensuring that the drive’s cascaded H-bridge topology operates at peak efficiency.
On the field bus side, the board supports integration with PROFIBUS DP and PROFINET IO communication protocols, allowing seamless data exchange with upstream Siemens SIMATIC S7-300 or S7-400 PLC systems. This connectivity enables the PLC to dynamically adjust drive parameters — such as acceleration ramps, deceleration curves, and energy recovery modes — based on real-time production demand signals. The result is a closed-loop maintenance planning system where motor speed is continuously matched to actual process load, eliminating the unplanned downtime associated with fixed-speed or manually adjusted drives.
For facilities that have deployed Siemens SENTRON PAC power monitoring devices or SICAM maintenance planning systems, the A5E01708486-equipped drive can feed real-time power consumption data back into the plant’s condition monitoring dashboard. This integration supports ISO 50001 maintenance planning compliance and provides the granular kWh-per-unit data needed for production efficiency benchmarking.
In servo-driven auxiliary systems adjacent to the MV drive, components such as the Siemens SINAMICS S120 servo drive and associated CU320-2 Control Unit may share the same PROFINET backbone, allowing coordinated motion and energy profiling across both MV and LV drive tiers. The Siemens ET 200SP distributed I/O modules further extend the control reach, enabling remote signal acquisition from sensors, encoders, and temperature monitors mounted directly on the motor or driven equipment.
HMI visibility is typically provided through a Siemens SIMATIC TP1200 Comfort Panel or equivalent operator interface, where plant engineers can monitor drive efficiency curves, review operating load trends, and configure operational-efficiency operating modes — all without interrupting production. This level of system transparency is essential for identifying inefficiencies before they escalate into unplanned downtime.
Maintenance and Replacement Notes
In real-world production environments — from cement grinding mills and water treatment pump stations to petrochemical compressor trains and steel rolling lines — the quality of signal control within an MV drive directly determines how much energy is consumed per ton of output. A degraded or failing signal control board introduces timing errors that force the drive to compensate with excess torque, increasing current draw and heat generation. Over time, this not only raises energy costs but accelerates wear on motor windings, bearings, and power cell capacitors.
Replacing a worn or faulty board with a genuine Siemens A5E01708486 restores the drive’s ability to execute precise speed ramps and maintain stable torque profiles under variable load conditions. In pump and fan applications — which account for a large share of industrial electricity consumption — even a 5% improvement in drive signal accuracy can translate to a 10–15% reduction in annual energy expenditure, depending on operating hours and load profile.
From a production line rhythm (takt time) perspective, a stable signal control board eliminates the micro-interruptions caused by signal faults or drive trips. Each unplanned stop in a continuous process line — whether in a paper mill, a chemical reactor feed system, or a mining conveyor — carries a cost that extends far beyond the unplanned downtimed during restart. Restoring signal integrity with the A5E01708486 keeps the line running at its designed cadence, protecting both throughput and product quality.
Predictive maintenance strategies also benefit directly from a properly functioning signal board. When the A5E01708486 is operating correctly, the drive’s diagnostic outputs — vibration signatures, current harmonics, thermal trends — are accurately captured and transmitted to the plant’s condition monitoring system. Facilities using Siemens SIMATIC WinCC SCADA or third-party predictive maintenance platforms can leverage this data to schedule maintenance during planned shutdowns rather than reacting to emergency failures, reducing both maintenance costs and energy losses associated with degraded equipment operation.
Every unit of the A5E01708486 supplied by ZYPLC undergoes functional testing and output verification prior to shipment, ensuring that the board performs to Siemens factory specifications from the moment it is installed. Combined with a warranty terms confirmed during quotation and reliable global inventory availability, this makes the A5E01708486 a low-risk, high-value replacement component for any facility operating Perfect Harmony MV drives.
Product Sourcing FAQ
Q1: How does the A5E01708486 contribute to operational stability in a Perfect Harmony MV drive system?
The A5E01708486 signal control board ensures that speed reference and torque command signals are processed and delivered to the drive’s power cells with high accuracy and minimal latency. This precision allows the Perfect Harmony drive to operate at the exact speed required by the process load — avoiding over-speed conditions, reducing reactive power, and eliminating the unplanned downtime caused by signal-induced torque oscillation. In variable-load applications such as pumps and fans, this translates directly to lower kWh consumption per operating hour.
Q2: Is the A5E01708486 compatible with both the GH180 and NXG variants of the Perfect Harmony drive?
The A5E01708486 is designed for use within the Siemens Perfect Harmony MV drive platform. Compatibility with specific drive variants (GH180, NXG, or earlier generations) depends on the drive’s firmware version and hardware revision. We recommend verifying the drive’s nameplate data and existing board revision before ordering. Our technical team can assist with cross-referencing your drive’s configuration to confirm fitment.
Q3: What is the recommended replacement procedure, and how long does installation take?
Board replacement should be performed by a qualified drive service engineer following Siemens’ documented maintenance procedures for the Perfect Harmony series. The drive must be fully de-energized and locked out before any board-level work is undertaken. Typical board swap time is 1–3 hours depending on drive cabinet configuration and site conditions. Post-installation, a functional test including signal verification and a no-load run is recommended before returning the drive to full production service.
Q4: What warranty and pre-shipment testing does ZYPLC provide for the A5E01708486?
All A5E01708486 units supplied by ZYPLC are covered by a warranty terms confirmed during quotation from the date of shipment. Each board is tested for functional output and signal integrity before dispatch. Units that do not meet performance benchmarks are not shipped. In the event of a warranty claim, ZYPLC provides replacement or repair support with documented RMA procedures. Contact our team at plc.sales@zyplc.com or +86 19859288691 for warranty inquiries.