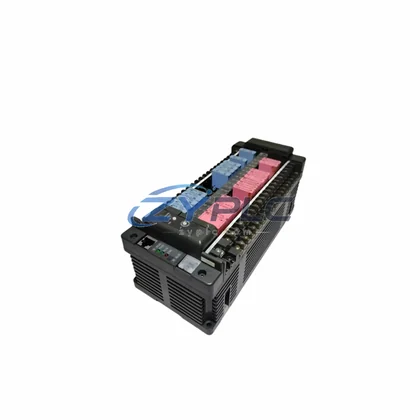
Rexroth VT-HNC100-C-30/P-S-00/000: Industrial Data Link for Smart Factory Axis Control
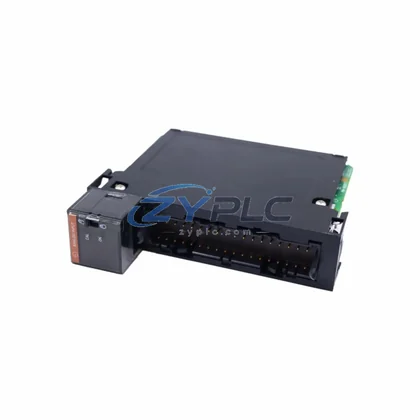
The Bosch Rexroth VT-HNC100-C-30/P-S-00/000 is a high-performance digital axis controller engineered for precision motion control and seamless industrial network integration within the VT-HNC100 Series. Designed to serve as the critical communication bridge between field-level devices and upper-level control systems, this controller enables real-time data exchange across complex automation architectures — from servo drives and hydraulic actuators to PLC controllers, HMI panels, and SCADA platforms.
In modern smart factory environments, the demand for deterministic, low-latency communication between motion controllers and supervisory systems has never been greater. The VT-HNC100-C-30/P-S-00/000 addresses this challenge by supporting the SERCOS (Serial Real-time Communication System) interface protocol, a fiber-optic-based industrial network standard purpose-built for high-speed, noise-immune motion control data transmission. This makes it an ideal fit for multi-axis synchronization tasks where microsecond-level timing accuracy is non-negotiable.
Whether deployed in hydraulic press lines, injection molding machines, metal forming equipment, or automated assembly systems, this Rexroth axis controller delivers the connectivity backbone that modern industrial sites require. Its integration capability with Bosch Rexroth’s broader IndraControl and IndraMotion ecosystems ensures that engineers can build scalable, future-ready automation networks without sacrificing performance or reliability.
Compatibility & Integration Notes
| Parameter |
Specification |
| SKU / Part Number |
VT-HNC100-C-30/P-S-00/000 |
| Brand / Manufacturer |
Bosch Rexroth |
| Series |
VT-HNC100 |
| Communication Protocol |
SERCOS (Serial Real-time Communication System) |
| Interface Type |
Fiber Optic SERCOS Ring / Digital I/O |
| Transmission Capability |
Real-time deterministic motion data, cyclic/acyclic communication |
| Network Compatibility |
SERCOS I/II, compatible with Rexroth IndraControl, IndraMotion platforms |
| System Application |
Hydraulic axis control, servo synchronization, PLC integration, SCADA/HMI connectivity |
| Product Type |
Digital Axis Controller |
| Origin |
Germany |
| Warranty |
warranty terms confirmed during quotation |
| Supply Status |
RFQ Available — shipment arranged after confirmation |
Connected Automation Data Flow
The VT-HNC100-C-30/P-S-00/000 sits at the heart of a layered industrial communication architecture. At the field level, signals originate from pressure sensors, position transducers, and flow measurement devices connected to the hydraulic or electromechanical actuator. These analog and digital signals are conditioned and fed into the axis controller, which processes them in real time using its onboard closed-loop control algorithms.
The controller communicates upstream via the SERCOS fiber-optic ring to a master PLC — typically a Bosch Rexroth IndraControl L65 or compatible IndraControl XM platform — which coordinates multi-axis motion sequences and manages interlocking logic across the production line. The SERCOS protocol ensures that position, velocity, torque, and status data are exchanged within deterministic cycle times, enabling precise synchronization between axes without communication jitter.
At the supervisory level, the IndraControl PLC interfaces with WinCC or InTouch HMI panels via Ethernet/IP or PROFINET, providing operators with real-time visualization of axis position, drive status, fault codes, and production counters. The HMI data feeds into a SCADA gateway — such as a Rexroth IndraMotion MLC or a third-party OPC-UA server — which aggregates data from multiple VT-HNC100 controllers across the plant floor and pushes it to the MES or cloud analytics layer.
For drive-level integration, the VT-HNC100-C-30/P-S-00/000 works in conjunction with Rexroth IndraDrive C or IndraDrive M servo drives, receiving torque and speed setpoints via the SERCOS interface and returning actual values for closed-loop verification. Remote I/O modules — such as the Rexroth Inline I/O system — extend the controller’s digital and analog I/O reach to distributed field devices without additional wiring complexity.
For remote diagnostics and predictive maintenance, the system supports integration with Rexroth ActiveCockpit or compatible edge gateway devices, enabling condition monitoring data — vibration signatures, thermal profiles, cycle counts — to be streamed to cloud dashboards for analysis. This end-to-end data flow, from sensor signal to cloud insight, exemplifies the connectivity value that the VT-HNC100-C-30/P-S-00/000 delivers in a fully networked smart factory.
Solving Data Isolation in Industrial Sites
One of the most persistent challenges in industrial automation is the fragmentation of communication protocols across different generations of equipment. Older hydraulic controllers may rely on proprietary analog interfaces, while newer PLC platforms demand digital fieldbus or Ethernet-based connectivity. The VT-HNC100-C-30/P-S-00/000 bridges this gap by providing a standardized SERCOS digital interface that can be integrated into both legacy and modern control architectures.
Data silos — where motion controllers, safety systems, and process controllers operate in isolation — are a major barrier to production transparency and OEE improvement. By connecting the VT-HNC100 axis controller into the plant-wide SERCOS or Ethernet network, engineers gain unified visibility into axis performance, fault history, and energy consumption data that was previously locked inside standalone controllers.
Remote monitoring becomes straightforward once the VT-HNC100-C-30/P-S-00/000 is networked: maintenance teams can access real-time axis diagnostics, review alarm logs, and perform parameter adjustments from a central control room or via secure remote access — eliminating the need for on-site intervention for routine diagnostics. This capability is especially valuable for multi-site manufacturers managing geographically distributed production lines.
System scalability is another key advantage. The SERCOS ring topology allows additional axis controllers, drives, and I/O nodes to be added to the network without disrupting existing communication. As production requirements evolve — new product variants, additional axes, higher throughput targets — the VT-HNC100 platform scales to meet them, protecting the initial automation investment and reducing future integration costs.
All units supplied by ZYPLC undergo pre-shipment functional verification, including communication interface testing and parameter integrity checks, ensuring that every VT-HNC100-C-30/P-S-00/000 arrives ready for immediate commissioning. Combined with a warranty terms confirmed during quotation and availability confirmed by RFQ availability for fast global dispatch, ZYPLC provides the supply chain reliability that industrial procurement teams depend on.
Industrial Connectivity FAQ
Q1: What communication protocol does the VT-HNC100-C-30/P-S-00/000 use, and is it compatible with my existing PLC?
The VT-HNC100-C-30/P-S-00/000 uses the SERCOS (Serial Real-time Communication System) fiber-optic protocol, which is natively supported by Bosch Rexroth IndraControl and IndraMotion PLC platforms. Compatibility with third-party PLCs depends on the availability of a SERCOS master interface card. For integration with PROFINET or EtherCAT-based systems, a protocol gateway module may be required — contact our technical team for application-specific guidance.
Q2: How does this controller handle communication latency in high-speed multi-axis applications?
The SERCOS interface operates with deterministic cycle times as low as 62.5 µs, making it suitable for high-speed, multi-axis synchronization tasks where communication jitter would cause positioning errors. The VT-HNC100-C-30/P-S-00/000’s onboard processing ensures that control loop execution and network communication are tightly synchronized, maintaining axis performance even under demanding dynamic conditions.
Q3: Can the VT-HNC100-C-30/P-S-00/000 be integrated into an existing SCADA or remote monitoring system?
Yes. Via the upstream PLC (e.g., Rexroth IndraControl), the axis controller’s data — position, velocity, fault status, cycle counts — can be made available to SCADA platforms via OPC-UA, PROFINET, or Ethernet/IP. This enables real-time monitoring, alarm management, and historical data logging within existing plant SCADA/HMI infrastructure without requiring hardware modifications to the axis controller itself.
Q4: What does the warranty terms confirmed during quotation cover, and how does ZYPLC verify units before shipment?
All VT-HNC100-C-30/P-S-00/000 units supplied by ZYPLC are covered by a warranty terms confirmed during quotation against manufacturing defects and functional failures. Prior to shipment, each unit undergoes a pre-delivery inspection that includes communication interface verification, firmware integrity check, and visual inspection for physical damage. Units are shipped with full export documentation, and expedited delivery options are available for urgent project requirements.