
ZYPLC Blog
Mitsubishi MELDAS and iQ-R Motion Spares: Board and Axis Evidence Before CNC Recovery
A CNC or motion-system outage often starts with a board alarm, axis following error, or communication issue that is difficult to separate under pressure. Mitsubishi MELDAS and iQ-R spare planning should connect the board, motion module, axis role, cable evidence, and recovery test. ZYPLC covered Rexroth and Pro-face in the latest posts, so today moves […]
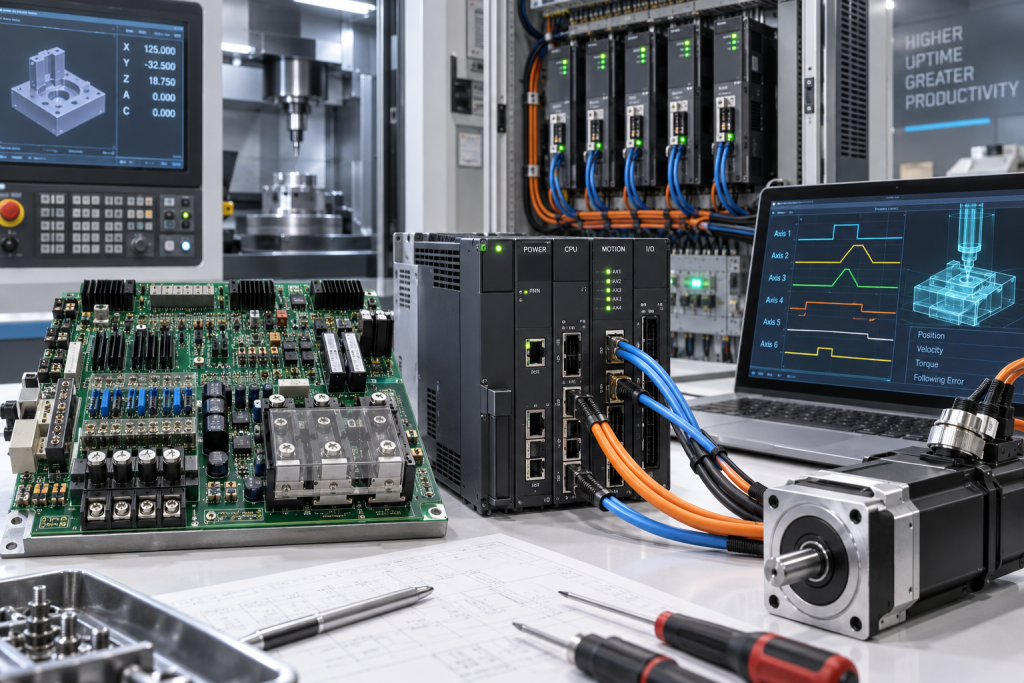
A CNC or motion-system outage often starts with a board alarm, axis following error, or communication issue that is difficult to separate under pressure. Mitsubishi MELDAS and iQ-R spare planning should connect the board, motion module, axis role, cable evidence, and recovery test.
ZYPLC covered Rexroth and Pro-face in the latest posts, so today moves into Mitsubishi motion and CNC board evidence without repeating yesterday’s servo-drive topic.
Identify The Axis And Control Board
Record CNC model, axis name, board number, motion module, drive amplifier, feedback path, SSCNET or field cable, parameters, fault code, and the machine function affected.
The first product reference checked before drafting was Mitsubishi GU-G04 GCU04AB Thyristor Control Board for MELDAS Systems. It belongs in the discussion because the article is about the same installed risk, not because a link is needed at the end of the page.
The second published reference was Mitsubishi RD77MS16 SSCNETIII/H Motion Module iQ-R Series. Using two real, public product pages gives maintenance and procurement a practical vocabulary for labels, suffixes, connectors, and acceptance evidence.
Motion Recovery Depends On More Than A Module
A board or motion module can be correct but still fail if parameters, cable type, feedback, servo amplifier status, safety inputs, or mechanical load are not checked.
Ask suppliers for actual photos, connector condition, tested status, accessory scope, board revision evidence, and any firmware or parameter-transfer concerns.
A spare request should be written like a compact engineering handover. It needs the installed part identity, cabinet location, accessories, field wiring, software or parameter dependency, observed symptom, and the test that decides whether the part is acceptable. Without that evidence, the buyer is forced to compare catalog names instead of recovery risk.
Acceptance Should Prove Controlled Axis Motion
After replacement, verify diagnostics, parameter load, network recognition, feedback state, servo enable, homing or jog test, following error, and operator approval.
If the axis remains blocked, review power, cable seating, encoder path, brake circuit, drive alarm, mechanical load, safety inputs, and CNC parameter compatibility.
The plant should also record what remains unknown. Firmware, backup files, licenses, calibration records, communication schedules, safety validation, and loop checks are site responsibilities. A supplier can confirm hardware identity and condition, but system readiness is proven only when the installed function passes the plant test.
Procurement Notes For Maintenance Teams
Ask for actual photos before approving shipment. Front labels, side labels, connector faces, terminal screws, rack position, LED state, daughter boards, batteries, cable tags, and accessory kits can reveal compatibility details that a one-line part number hides.
Separate emergency recovery from planned inventory. An emergency purchase may accept narrower evidence and faster freight, while a shelf spare should have cleaner documentation because it may be used by a different shift months later.
Condition terms should be specific. Factory sealed, new surplus, refurbished, repaired exchange, tested used, and untested used carry different risk. The RFQ should state which conditions are acceptable and what test evidence must accompany the offer.
Do not treat similar modules as automatic substitutes. Older PLC, DCS, SIS, HMI, drive, motion, robot, and condition-monitoring families often change by suffix, firmware, termination, memory, channel isolation, communication option, or cabinet depth.
Receiving inspection should repeat the sourcing evidence check. Compare the delivered item to the approved photos, confirm accessory scope, inspect connectors and terminals, record serial or revision details, and decide whether the part goes to stores, bench test, or immediate installation.
If a substitute is proposed, define the engineering review before purchasing releases the order. The reviewer should check fit, function, firmware or parameter impact, communication behavior, field wiring, safety consequence, and rollback plan.
For multisite groups, use a common RFQ format but allow local acceptance rules. A utility pump, turbine train, safety loop, valve skid, motion axis, robot cell, and operator panel do not carry the same consequence, even when the part numbers look routine.
A useful blog article for engineers should help the reader do the next practical step. That is why today’s topic is tied to real published product pages, current industry monitoring, and the evidence needed to move from research to a quote.
The best inquiry is short but complete: brand, full model, quantity, acceptable condition, installed role, photos, failure symptom, deadline, destination, and the acceptance test. That information reduces rework and makes supplier answers easier to compare.
Keep the final record with the spare. Product link, supplier evidence, photos, test notes, and acceptance status become valuable when the same platform fails again or when management asks why modernization should be funded.
The search angle also matters. Engineers may search by model number, but purchasing teams often search by family name, system name, or failure mode. A good article and a good RFQ should support both paths without stuffing keywords or forcing irrelevant products into the conversation.
When official support is limited, the quality of the installed evidence becomes even more important. Legacy hardware can often be kept reliable, but only when the site can prove what is installed, what is interchangeable, and what test will protect production after replacement.
FAQ
What must match on a Mitsubishi motion spare?
Match board or module identity, axis role, cable interface, parameter needs, revision concern, diagnostics, and recovery test.
Why include CNC and axis evidence?
The same board can support different machine roles, and acceptance depends on the axis function it restores.
What should procurement send?
Send labels, board photos, axis name, cable photos, fault code, parameter status, condition requirement, and deadline.
What proves recovery?
Clean diagnostics, recognized motion network, loaded parameters, stable feedback, successful jog or homing, and approved machine testing.
Send ZYPLC the Mitsubishi board labels, iQ-R motion module evidence, axis details, cable photos, fault code, and recovery deadline. We can help prepare a motion spare RFQ.
© 2026 ZYPLC. All rights reserved. Official Website: https://zyplc.com Inquiry: sales@zyplc.com | WhatsApp/Tel: +86 18359293191